A specialist website by Oxford Industrial Automation

UK robot & vision integration · 01865 416830

Defect containment

Automated reject handling systems

Turn an inspection decision into proven physical containment. Reject timing, mechanism, tracking, confirmation and collection are engineered around product behaviour and line risk.

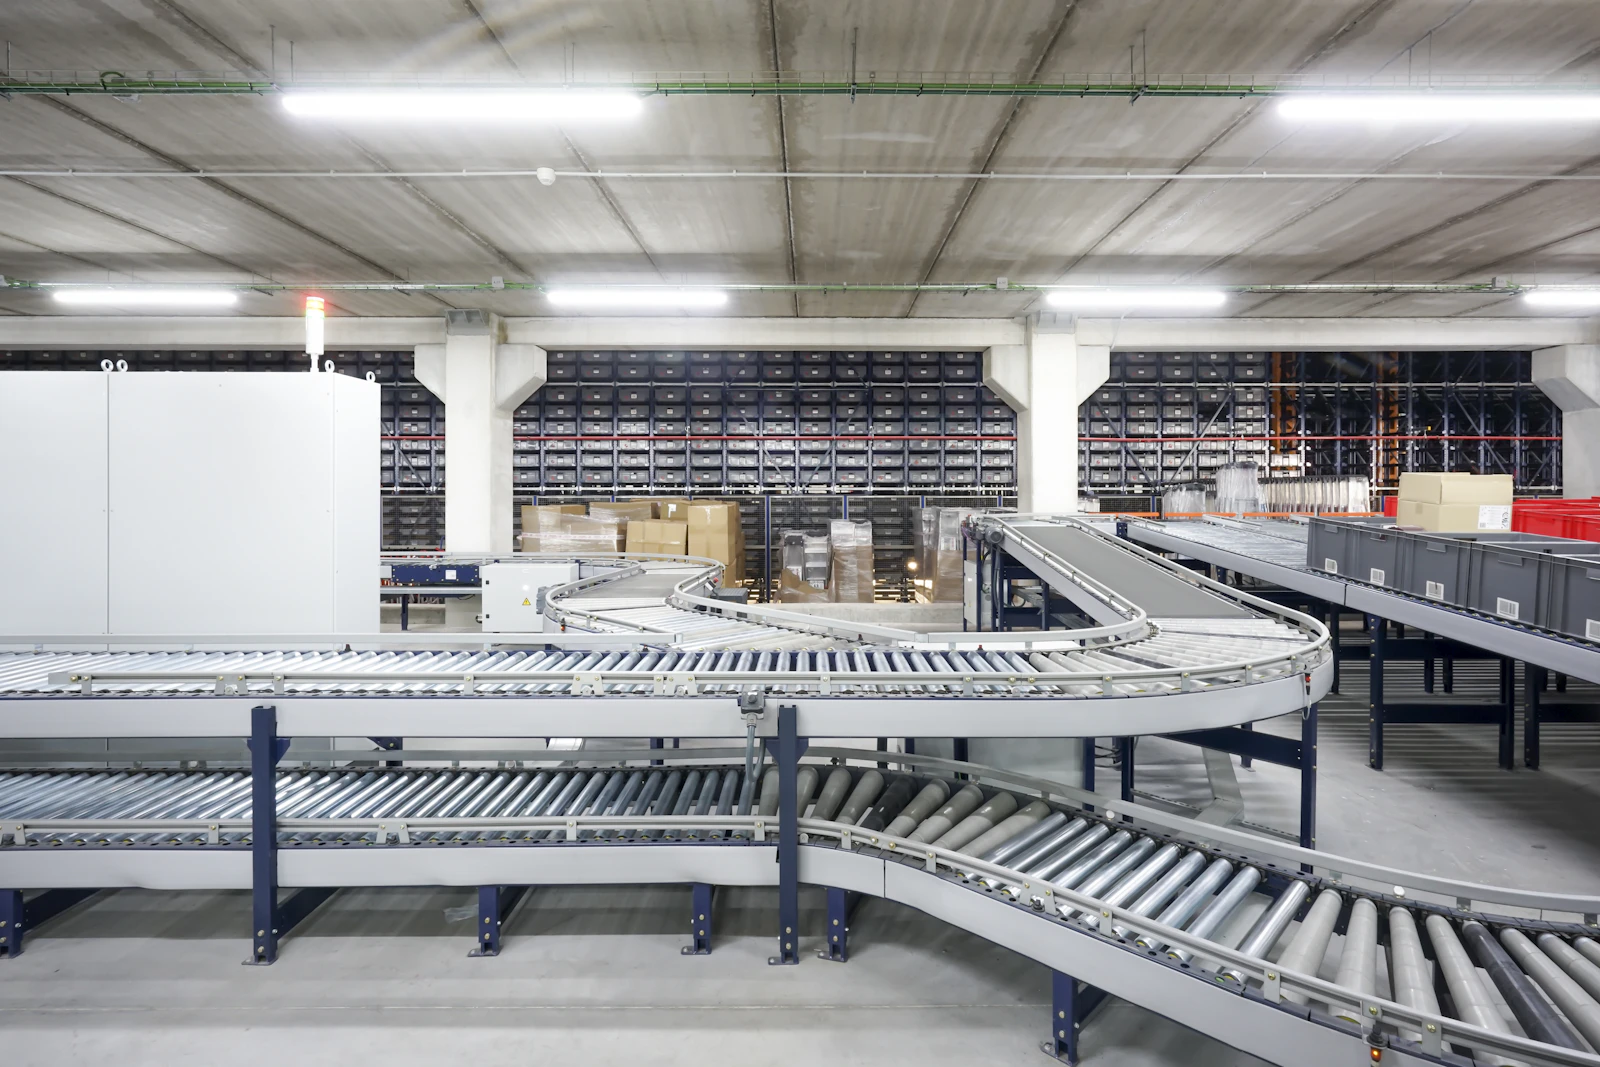
Curved roller conveyors and storage bins in a warehouse.
MechanismsAir, pusher, drop gate, diverter, servo or robot
ProofReject fired, product removed and container available
FaultAlarm, controlled stop or safe product diversion
01 / Engineering focus

Match the reject method to the product

Product mass, speed, stability, fragility and spacing determine whether a simple divert is appropriate or a controlled robotic removal is required.

  • Air blast for suitable light, stable products
  • Pusher and sweep mechanisms
  • Drop-flap and retracting-belt arrangements
  • Lane diverters and servo routing
  • Robot pick for controlled or classified rejects
02 / Engineering focus

Confirmation closes the control loop

The system should know whether the reject action achieved its purpose. Downstream sensors, timed windows and reject-container monitoring can create a defined response when containment is not confirmed.

  • Reject confirmation sensing
  • Full-bin, bin-present and access monitoring
  • Locked collection for controlled processes
  • Counters by reject reason and batch

System sequence

Engineer the complete decision loop.

Every stage is tested against the product, timing, interfaces and agreed response.

01

Track

Maintain the decision against the correct physical item.

02

Remove

Act within the available window without disturbing good product.

03

Confirm

Verify that the affected item left the accepted flow.

04

Contain

Manage collection, access, full-bin and fault response.

Typical applications

Where this capability can fit.

Final suitability and performance are confirmed only after review of the complete production application.

Inspection reject stations
No-read diversion
Multi-grade sorting
Robot reject pick
Confirmed containment
Reject count reporting

Application questions

What manufacturers ask.

These answers provide a starting point. Product trials and line data determine the project specification.

Which reject mechanism is best?

There is no universal answer. Product weight, shape, line speed, spacing, acceptable impact and available space determine the most reliable method.

How is the correct product rejected after the camera?

The control system tracks the inspection result through distance, encoder movement, pockets or product registration until the item enters the reject window.

Can the system stop if rejection is not confirmed?

Yes. A missing confirmation can trigger an alarm, controlled stop or alternative diversion according to the agreed risk and operating philosophy.

Start with the production task

Show us what the system needs to see and move.

Use the project brief form, or email product photos or video with the target output, current layout and required decision. We will define the next technical step.

Project brief